SAMPLE
Dongguan Guangyi Hardware Factory
2nd Floor, Hongfu Building, No. 45 Lianma Road, Dalingshan Town, Dongguan, Guangdong 523129, China
2nd Floor, Hongfu Building, No. 45 Lianma Road, Dalingshan Town, Dongguan, Guangdong 523129, China
CMM INSPECTION REPORT
First Article Inspection · Dimensional & Geometric
SAMPLE REPORT
- Report no.
- GY-FAI-260910-SAMPLE
- Date
- 10 Sep 2026
- Customer
- (customer name withheld)
- Customer PO
- PO-XXXXXX
- Part name
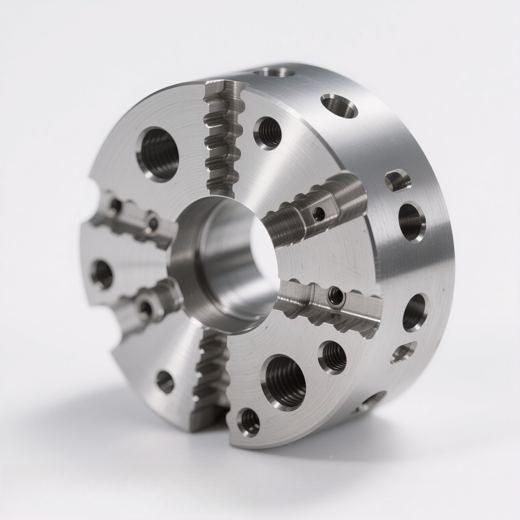
- Chuck body, 4-slot
- Part no. / rev
- SAMPLE-4120-01 · Rev C
- Material
- Stainless steel 303 (ASTM A582)
- Lot / sample
- Lot 26-0910 · 1 of 25 pcs (first article)
- Process
- CNC turned + 4-axis milled, tapped, deburred
- Instrument
- Bridge-type CMM, touch-trigger probe, ruby stylus 2 mm
- Calibration
- Calibration valid to 03/2027 (cert on file)
- Environment
- 20.4 °C / 51 % RH · part soaked 4 h
- Datum scheme
- A = rear face · B = Ø bore · C = slot 1 centre plane
- Units
- inch (drawing units) · mm shown in brackets
Measurement results
| # | Feature / characteristic | Nominal | Tolerance | Measured | Deviation | Result |
|---|---|---|---|---|---|---|
| 1 | Ø Bore (Datum B) | 1.2500[31.750] | +0.0005 / −0.0005 | 1.2503[31.758] | +0.0003 | PASS |
| 2 | Ø Outside diameter | 3.1500[80.010] | +0.0020 / −0.0020 | 3.1491[79.987] | -0.0009 | PASS |
| 3 | Overall thickness | 1.1800[29.972] | +0.0020 / −0.0020 | 1.1809[29.995] | +0.0009 | PASS |
| 4 | Ø Counterbore, 4× | 0.4375[11.112] | +0.0020 / −0.0000 | 0.4386[11.140] | +0.0011 | PASS |
| 5 | Counterbore depth, 4× | 0.3100[7.874] | +0.0050 / −0.0050 | 0.3084[7.833] | -0.0016 | PASS |
| 6 | Slot width, 4× (serrated) | 0.3750[9.525] | +0.0010 / −0.0000 | 0.3758[9.545] | +0.0008 | PASS ▲ |
| 7 | Slot depth from face | 0.6250[15.875] | +0.0030 / −0.0030 | 0.6238[15.845] | -0.0012 | PASS |
| 8 | Bolt circle Ø, 8× M8 holes | 2.6000[66.040] | +0.0020 / −0.0020 | 2.6007[66.058] | +0.0007 | PASS |
| 9 | Ø Cross-hole, 4× | 0.1875[4.762] | +0.0015 / −0.0000 | 0.1881[4.778] | +0.0006 | PASS |
| 10 | Chamfer, bore edge | 0.0300[0.762] | +0.0100 / −0.0100 | 0.0334[0.848] | +0.0034 | PASS |
| 11 | ⌖ Position, 8× M8 holes to A|B|C | 0.0000[0.000] | 0.0040 max | 0.0021[0.053] | 0.0021 | PASS |
| 12 | ⌖ Position, 4× counterbores to A|B|C | 0.0000[0.000] | 0.0040 max | 0.0027[0.069] | 0.0027 | PASS |
| 13 | ⟂ Perpendicularity, bore B to A | 0.0000[0.000] | 0.0010 max | 0.0004[0.010] | 0.0004 | PASS |
| 14 | ⏥ Flatness, rear face A | 0.0000[0.000] | 0.0010 max | 0.0003[0.008] | 0.0003 | PASS |
| 15 | ∥ Parallelism, front face to A | 0.0000[0.000] | 0.0015 max | 0.0009[0.023] | 0.0009 | PASS |
| 16 | ◎ Runout, OD to B | 0.0000[0.000] | 0.0020 max | 0.0011[0.028] | 0.0011 | PASS |
| 17 | Thread M8×1.25-6H, 8× | M8×1.25-6H | — | GO / NO-GO gauge | — | PASS |
| 18 | Surface finish Ra, faces | 32 µin max | — | 18 µin | −14 µin | PASS |
18Characteristics checked
18In tolerance
0Out of tolerance
ACCEPTDisposition · release run
▲ = within tolerance but using more than 80 % of the band; flagged to the machinist before the production run continues.
Positions reported as diameter, RFS, per ASME Y14.5-2018. Threads checked with GO / NO-GO gauges. Ra measured by an independent test house, cut-off 0.03 in. Values in brackets are mm.
Results apply only to the item(s) inspected. Measurement uncertainty is not included in the reported values.
This is a sample document showing the format of the inspection report that ships with a GY Machining first article. Part, customer and measured values are illustrative and do not describe a real order.
Inspected byQC inspector · 10 Sep 2026
Reviewed byBill · Engineering Manager
Released byWill · General Manager